Borax Pentahydrate
Borax Pentahydrate is a versatile chemical used in various applications, particularly in food processing and preservation. This product is supplied by Kivi Chemicals in 25kg packages, ensuring quality and reliability for your needs.
Chemical Properties

Borax Pentahydrate
Brand: Kivi Chemicals·Manufactured by: Kivi Chemicals
Borax Pentahydrate is a versatile chemical used in various applications, particularly in food processing and preservation. This product is supplied by Kivi Chemicals in 25kg packages, ensuring quality and reliability for your needs.
Product Introduction
Borax Pentahydrate, also known as ETIBOR-48, is a sodium borate compound recognized for its multifaceted applications in the food and beverage industry. Sourced and supplied by Kivi Chemicals, this product is essential in various food processing methods, particularly for its role in food preservation and pH regulation. With stringent quality standards, Borax Pentahydrate meets the requirements set forth by the Food Chemicals Codex (FCC) and has received approval from the Joint FAO/WHO Expert Committee on Food Additives (JECFA) for food use. This makes it an invaluable resource for manufacturers looking to enhance product safety and stability in their offerings across Kenya, Uganda, Tanzania, and the wider East African region.
Detailed Product Overview
Borax Pentahydrate, with the chemical formula Na2B4O7.5H2O, is a white crystalline solid primarily composed of sodium, boron, and oxygen. It boasts a molecular weight of 382.37 g/mol and a density of 1.73 g/cm³. The compound is characterized by its high solubility in water, making it versatile for various aqueous applications. The product meets a minimum purity of 99.0%, which is crucial for maintaining consistency and quality in sensitive processes. Its pH range of 7.5 to 9.5 in a 1% solution makes it ideal for applications requiring precise pH regulation. With a melting point of 75 °C, Borax Pentahydrate remains stable under standard industrial conditions, ensuring reliability in a wide range of uses. In industrial applications, Borax Pentahydrate is predominantly used in food preservation and pH regulation within the food and beverage industry. Its role as a buffering agent ensures that products maintain their intended acidity, which is essential for both flavor and preservation. Additionally, it finds use in cosmetic formulations and pharmaceutical applications, where its chemical stability and purity are critical. The compound's solubility and stable crystalline form make it easy to incorporate into various formulations, enhancing product performance. Its ability to act as a preservative extends the shelf life of food products, which is particularly valuable in the East African market where supply chain challenges can affect product availability. When sourcing Borax Pentahydrate, it is important to verify that the product conforms to food-grade standards, specifically the FCC standards, which ensure its suitability for food applications. The buyer should confirm the purity level of 99.0% minimum and check the moisture content, which should not exceed 5.0%. These specifications are crucial for maintaining product efficacy and safety in food applications. It is also advisable to ensure that the product's appearance is consistent with a white crystalline solid, as deviations can indicate contamination or degradation. Buyers should request a certificate of analysis to verify these parameters upon receipt. Handling and storage of Borax Pentahydrate require adherence to standard safety protocols due to its classification as a chemical substance. It should be stored in a cool, dry place, away from incompatible materials, to maintain its stability. The product is supplied by Kivi Industrial Chemicals Limited in 25 kg polypropylene bags, which provide durability and protection during transport and storage. These bags are designed to withstand the rigors of industrial handling, ensuring that the product remains uncontaminated until use. As with all chemical products, it is important to consult the Material Safety Data Sheet (MSDS) for detailed handling instructions and to ensure compliance with local regulations regarding chemical storage and transport.
Applications & Uses
Food Preservation
Borax Pentahydrate is utilized in food preservation processes, acting as a natural preservative that inhibits microbial growth and extends shelf life. It is especially effective in processed foods, ensuring safety and quality.
pH Regulation in Beverages
In the beverage industry, Borax Pentahydrate serves as a pH stabilizer, helping to maintain the desired acidity levels in soft drinks and other beverages. This contributes to flavor stability and product consistency.
Cosmetic Formulations
Beyond food applications, Borax Pentahydrate is also used in cosmetic formulations. It acts as a buffering agent, helping to stabilize pH levels in creams and lotions, enhancing product efficacy.
Pharmaceutical Applications
Borax Pentahydrate is included in some pharmaceutical formulations for its antiseptic properties and ability to stabilize active ingredients, making it valuable in the production of various medicinal products.
Industries Served
Benefits & Advantages
Borax Pentahydrate offers numerous benefits for East African buyers in the food and beverage sector. Its high purity level (99.0% Min) ensures that manufacturers can rely on its quality for food applications, meeting regulatory standards such as FCC and JECFA. The versatility of Borax Pentahydrate allows it to be used in various processes, from food preservation to pH regulation, enhancing product safety and extending shelf life. Additionally, its role in cosmetic formulations and pharmaceuticals highlights its multifunctionality, making it a cost-effective choice for businesses looking to streamline their ingredient sourcing. Kivi Chemicals provides reliable supply chains, ensuring that buyers have access to Borax Pentahydrate when needed, thus maintaining production efficiency.
Packaging & Bulk Supply
Kivi Chemicals supplies Borax Pentahydrate in 25 kg polypropylene bags, designed for easy handling and storage. This packaging format is ideal for both small-scale and large-scale operations, facilitating bulk purchases while ensuring product integrity during transport and storage.
Storage & Handling
To maintain the quality of Borax Pentahydrate, it should be stored in a cool, dry place away from direct sunlight and moisture. The packaging should remain sealed until use to prevent contamination. When handling the product, it is advisable to wear appropriate personal protective equipment, such as gloves and safety goggles, to minimize exposure. Ensure that any spills are cleaned promptly, and dispose of waste materials according to local regulations.
External References & Further Reading
Technical Specifications
| EC No. | 215-540-4 |
| Purity | 99.0% Min |
| CAS No. | 12179-04-3 |
| Density | 1.73 g/cm³ |
| INDEX No. | 005-011-01-1 |
| Appearance | White crystalline solid |
| Flash Point | N/A |
| Melting Point | 75 °C (167 °F) |
| Moisture Content | ≤ 5.0% |
| Molecular Weight | 382.37 g/mol |
| pH of 1% Solution | 7.5 - 9.5 |
| Solubility in Water | Soluble |
Safety & Handling Guidelines
Not classified as hazardous under GHS
Borax Pentahydrate is not classified as hazardous under GHS regulations, which indicates a favorable safety profile for users. However, it is essential to handle the compound with care. Personal protective equipment (PPE) such as gloves and goggles should be worn to avoid irritation. In case of contact with eyes or skin, rinse thoroughly with water. If ingested, seek medical attention. Ensure to keep the product away from incompatible materials to prevent any adverse reactions.
Regulatory Compliance & Standards
Ready to order Borax Pentahydrate?
Our supply desk responds with pricing and lead times, usually within one business day.
Frequently Asked Questions
What is Borax Pentahydrate used for?
Borax Pentahydrate is commonly used in food preservation, pH regulation in beverages, and cosmetic formulations. It also has applications in pharmaceuticals.
Is Borax Pentahydrate safe for food use?
Yes, Borax Pentahydrate meets FCC standards and has been approved by JECFA for food applications, ensuring its safety for use in food processing.
How should Borax Pentahydrate be stored?
It should be stored in a cool, dry place, away from moisture and direct sunlight, and kept in a sealed container until use.
What are the handling precautions for Borax Pentahydrate?
While not classified as hazardous, it is recommended to wear personal protective equipment such as gloves and goggles when handling Borax Pentahydrate.
Can Borax Pentahydrate be used in cosmetic products?
Yes, it is used in cosmetic formulations as a buffering agent to stabilize pH levels.
What is the purity level of Borax Pentahydrate?
Borax Pentahydrate has a purity level of 99.0% minimum.
What is the packaging size for Borax Pentahydrate?
Kivi Chemicals supplies Borax Pentahydrate in 25 kg polypropylene bags.
What industries use Borax Pentahydrate?
It is used in food and beverage manufacturing, cosmetics, and pharmaceuticals.
Related Formulations
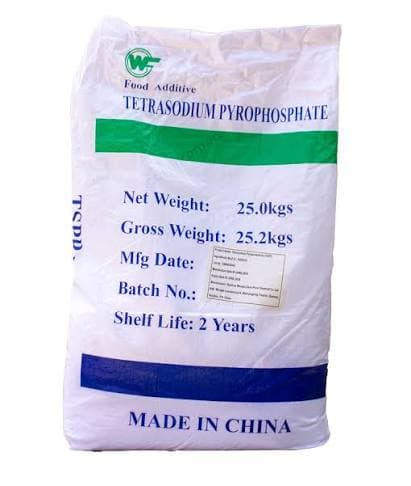
Tetrasodium Pyrophosphate ( TSPP )
Tetrasodium Pyrophosphate is a food additive commonly used as an emulsifier and thickening agent. It comes in a 25 kg package, ideal for various food processing applications.
WhatsApp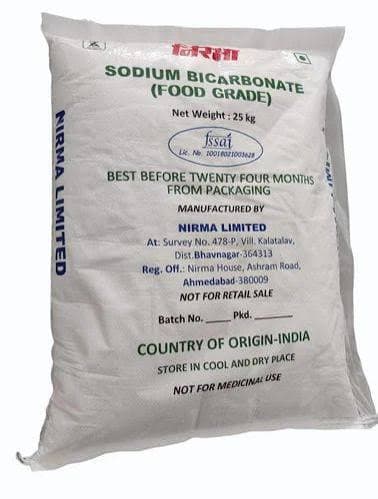
Sodium Bicarbonate
Sodium Bicarbonate, also known as baking soda, is a versatile food-grade chemical used in various applications including baking, pH regulation, and as a leavening agent.
WhatsApp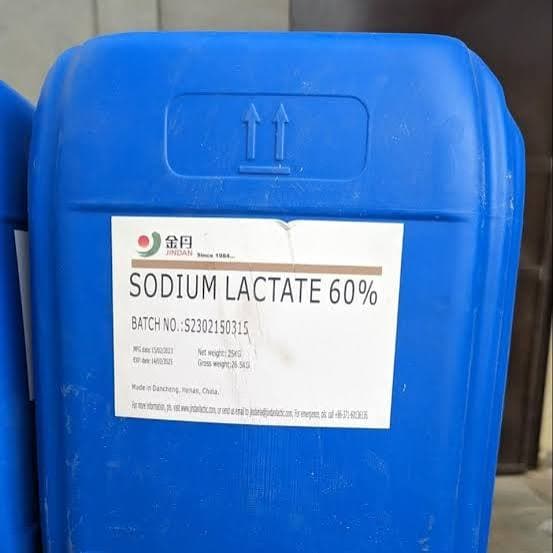
Sodium Lactate 60%
Sodium Lactate 60% is a versatile compound used primarily in food and beverage applications. It is available in a 250 kg net weight packaging, ensuring ample supply for various industrial needs.
WhatsApp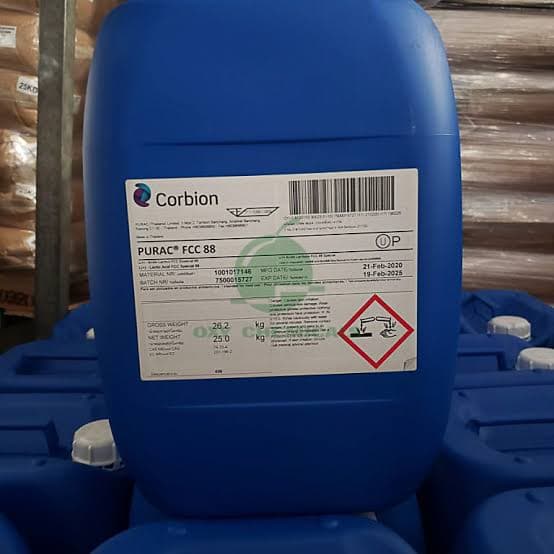
PURAC® FCC 88 Lactic Acid 81% (Excel grade)
PURAC® FCC 88 is a food-grade lactic acid product from Corbion, ideal for various applications in the food industry.
WhatsApp
Lactic Acid 80% Feed Grade
YUKATA Lactic Acid 80% Feed Grade is a high-purity organic acid suitable for various industrial applications, particularly in animal feed formulations.
WhatsApp
Lactic Acid 80% Food Grade
Lactic Acid 80% Food Grade is a versatile ingredient used in food processing and preservation. It is recognized for its safety and efficacy in various applications.
WhatsApp
Sodium Benzoate (moodle)
Sodium Benzoate is a widely used preservative in food and beverage industries. Known for its antimicrobial properties, it helps extend shelf life and maintain product quality.
WhatsApp
Sodium Benzoate(granule)
Sodium Benzoate is a widely used preservative in the food and beverage industry, helping to inhibit the growth of mold, yeast, and bacteria. It is supplied by Kivi Chemicals in convenient packaging for various applications.
WhatsApp